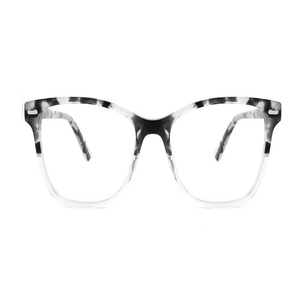
Bio-Acetate
Engineered to withstand rigorous global retail performance tests. Available for private-label white-labeling, brand customization, and high-volume turnkey procurement direct from audited export facilities.
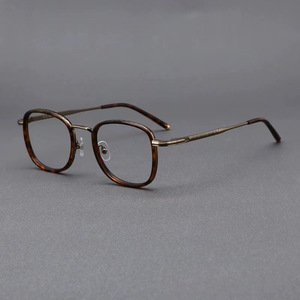
Combining European ergonomic research with precision manufacturing in South China's premier optical industrial clusters, we deliver verifiable engineering excellence and scalable supply reliability.
Rooted in optical benchwork since the 1950s, our founding team mastered precision lens grinding and optical centering before developing proprietary manufacturing workflows. This clinical heritage ensures that every chassis matches exacting ophthalmic glazing standards.
We eliminate conventional micro-screw failure points. Our proprietary Screwless Hinges and Active Return Hinges deploy calibrated interlocking geometry and high-tensile spring mechanisms to maintain constant temple torque over 25,000 continuous opening cycles.
Operating from Hong Leong Technology Park in Shenzhen, our export facilities leverage high-speed multi-axis CNC routers, automated ultrasonic tumbling barrels, and Class 10,000 dust-free robotic coating lines for micron-level dimensional tolerances.
Procuring optical frames from China requires precise knowledge of base materials, galvanic coatings, and machining tolerances. A major issue in cross-border eyewear procurement is discrepancies between initial prototype resin grades and high-volume injection stock. Below is an engineering overview of our standardized production substrates.
| Substrate Classification | Material Specification | Tensile / Flexural Rating | Machining & Glazing Application |
|---|---|---|---|
| High-Density Bio-Acetate | Cellulose acetate derived from sustainable cotton linters and wood pulp (>68% bio-based content). Plasticizer: bio-based diethyl phthalate alternatives. | Shore D Hardness: 82–86. Flexural Modulus: 2,400 MPa. |
Dry 5-axis CNC router profiling. Accepts cold snap-in and heat-assisted prescription lens insertion (60°C warm air bench). Exceptional luster retention after 72-hour walnut barrel polishing. |
| Aerospace Beta-Titanium | Ti-15V-3Cr-3Sn-3Al or Grade 5 Titanium alloys. High yield strength, zero nickel content, extreme biocompatibility. | Yield Strength: ≥880 MPa. Density: 4.51 g/cm³. |
Laser micro-welding in argon-purged chambers. Ideal for rimless tension-mount systems and ultra-thin flexible wire fronts. Finished with IP (Ion Plating) vacuum deposition. |
| Polyamide Memory TR-90 | Original Swiss EMS Grilamid TR-90 transparent polyamide. Ultra-low moisture absorption, high heat distortion resistance. | Tensile Strength at Yield: 65 MPa. Izod Impact: No break at 23°C. |
Precision hydraulic injection molding. Engineered for flexible children's eyewear and performance wrap sport shields. Resistant to perspiration, alcohol, and cosmetic oils. |
| Nickel-Free Monel & Stainless | SUS304/SUS316 medical-grade stainless steel ribbon wire with lead-free solder points. Nickel-release <0.5 μg/cm²/week. | Elongation at Break: ≥35%. Corrosion: >120h salt spray. |
High-speed progressive die stamping and CNC contour forming. Excellent structural ductility for easy optical dispensing and pantoscopic angle adjustment. |
In conventional children's eyewear, lateral torque from routine playground impacts breaks hinge knuckles and strips barrel screws. To address this, our EYELET pediatric series uses a flexible nylon-string soft-lock connection rather than rigid metal hinge pins.
This design prevents temporal trauma to child wearers, protects temple integrity, and minimizes warranty returns for dispensing optometrists. Coupled with lightweight TR-90 fronts, it ensures consistent optical center centering across wide pupillary distance ranges.
How shifts in environmental regulations, regional manufacturing specializations, and consumer demographics are transforming eyewear contract manufacturing.
Strict European Union green procurement directives are driving the phase-out of traditional petroleum-based acetate sheets. Leading importers now require certified biodegradable cellulose polymers with closed-loop monomer recovery, verified by ISO 14855 compostability assays.
Optical buyers are increasingly specifying frames ready for smart components. Custom factory runs include internal CNC routing for micro-circuitry, bone conduction transducers, and concealed battery bays within standard temple volumes, avoiding clunky silhouettes.
Global buyers are moving away from broad sourcing toward regional specialists: Shenzhen for premium Mazzucchelli acetate and CNC titanium; Danyang for high-volume CR-39/polycarbonate lenses and value frames; and Wenzhou for rapid metal stamping and mid-tier export programs.
Large, slow-moving container orders are giving way to agile, data-driven batch runs. Importers maintain centralized inventory buffers of polished front chassis, while laser custom logos, custom pad printing, and localized lens glazing are triggered in flexible 300-piece runs.
A single frame failure during prescription lens insertion can compromise an optical retailer's customer loyalty. Our export production lines follow rigorous international testing standards, providing full batch traceability and authenticated third-party test reports.
Every export shipment includes verified technical documentation for smooth customs clearance and regulatory compliance across all target jurisdictions:
Direct technical answers to the most common questions raised by optical chains, private-label directors, and wholesale buyers.
For custom acetate CNC models, our standard production run starts at 300 pieces per model (divided into 2–3 colorways). For bespoke injection-molded TR-90 or titanium chassis requiring new tooling, MOQ ranges from 600 to 1,200 pieces. For in-stock catalog silhouettes with private-label laser customization, we support pilot initial orders from 100 units.
Initial rapid 3D physical modeling and CNC mock-up samples are delivered within 10 to 14 working days. Finished counter-samples in targeted production acetate or metal take 25 to 30 days. Full-scale batch production takes approximately 45 to 60 days following sample sign-off, depending on plating complexity.
Yes. Our in-house R&D engineering department handles full CAD-to-CAM translation for specialized mechanical hardware. We routinely build screwless, spring-tensioned, active-cam, and flexible joints under strict non-disclosure agreements (NDAs) to protect your intellectual property.
We source raw laminated sheets exclusively from verified global manufacturers like Mazzucchelli 1849 and top-tier domestic producers. Acetate batches are cross-checked using digital spectrophotometers to maintain delta-E color variance under 0.8, ensuring reliable color matches between restocking cycles.
Frames are supplied by default with 1.50 or 1.56 index optical-grade acrylic (PMMA) demo lenses, precision-cut to prevent rim shrinkage during international shipping. We can also glaze finished blue-light blockers, polarized sun lenses, or prescription RX orders directly at our facility.
We welcome both scheduled on-site client inspections and accredited third-party quality audits (e.g., SGS, Bureau Veritas, TUV Rheinland). Complete inspection access is granted to raw material warehouses, CNC cleanrooms, tumbling facilities, manual alignment benches, and packaging lines.
Connect with our technical engineering team in Shenzhen and Singapore to review your CAD drawings, request material swatch rings, or plan private-label production schedules.
Contact Us